How Connected Systems Drive Smarter Production
Every pharmaceutical batch starts as a plan and ends as a record. In between sit raw materials, equipment, operators, quality checks, and a long documentation trail. When the systems managing each stage don’t communicate, someone ends up reconciling the gaps by hand, and that is where delays, duplicated effort, and stressful audits begin.
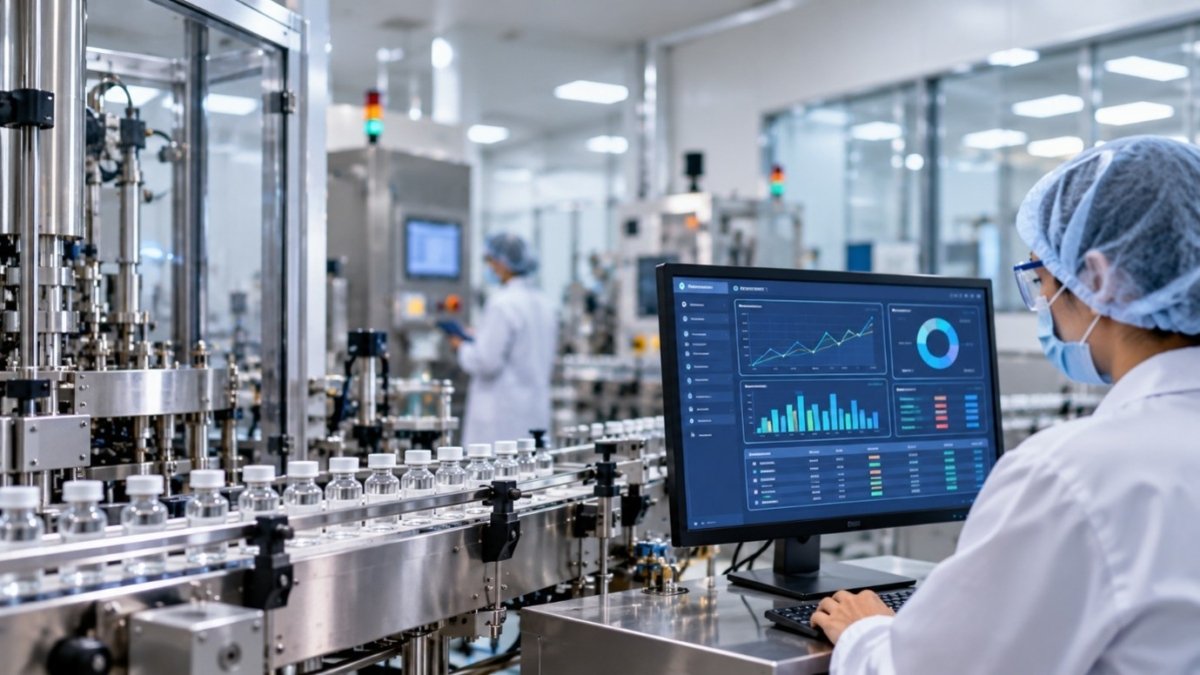
That is why digital manufacturing in pharma increasingly means connecting Enterprise Resource Planning (ERP), Manufacturing Execution Systems (MES), and manufacturing analytics. Linking planning, production, and performance analysis improves information flow, strengthens traceability, and gives teams a firmer basis for operational decisions.
ERP and MES Integration: Bridging Planning and the Shop Floor
ERP is the business backbone of a pharmaceutical site. It handles production planning, procurement, inventory, material requirements, and order management, so it knows what needs to be made, by when, and whether materials are available. What it doesn’t show is what is happening on the line right now.
That is the role of MES. It turns a plan into guided execution by leading operators through defined workflows, capturing material consumption, recording production activities, and maintaining batch-level information. In regulated environments, MES also supports electronic batch records (eBR), in-process controls, and traceability, replacing paper records that are slow to review and easy to get wrong.
With ERP MES integration, a process order released in ERP flows into MES for execution. Confirmations, actual material consumption, and batch status flow back. Planning, production, and quality teams work from the same version of events, with far less re-keying. Integration won’t remove every manual step, but it removes the duplicate ones.
How Pharmaceutical Manufacturing Analytics Shows What Really Happened
ERP shows schedules, inventory, and order status. MES shows what happened on the floor, step by step. Analysed together, they let teams compare plan against reality across the metrics that matter most:
- Cycle time: actual versus planned production duration
- Equipment downtime: stoppages that disrupt schedules
- Yield and material consumption: output and usage against expectations
- OEE in pharma: equipment availability, performance, and quality combined
- Batch performance: trends and recurring deviations
Consider repeated delays on a tablet compression line. ERP reports that the order finished late, but not why. MES data may reveal repeated stoppages, extended changeovers, or batches waiting between process steps. With both views side by side, the investigation starts from evidence instead of assumption, and the fix targets the cause rather than the symptom.
The same approach applies to yield variation and recurring deviations. With good data quality, teams can shift from explaining what went wrong to spotting early patterns before a batch is affected.
What to Get Right Before You Integrate ERP and MES
Connecting systems takes more than building interfaces. A few foundations decide whether the result is dependable.
Master data comes first: Materials, bills of materials, recipes, units of measure, and equipment identifiers must match across systems. If they don’t, every report built on top inherits the mismatch. Just as important, define which system owns each data element, when it moves, and how exceptions are handled.
Data integrity is the next layer: Records should stay accurate, complete, and traceable as they move between applications. The ALCOA+ principles (attributable, legible, contemporaneous, original, accurate, and more) are a useful yardstick, and audit trails should survive every handoff.
Regulation shapes the design from day one: FDA 21 CFR Part 11 covers electronic records and signatures within its scope, while EU GMP Annex 11 addresses computerized systems in GMP environments. Requirements depend on each system’s intended use, but validation, access controls, and audit trails are rarely optional.
Security and availability matter just as much: Plan for access permissions, cybersecurity, interface failures, and recovery, with clear handling for missing, delayed, or rejected data so issues don’t go unnoticed.
Finally, design for how the site really works. Shift changes, material release, deviation handling, and batch review all affect how information should move between systems.
A Practical Way to Start
Most manufacturers don’t need to connect everything at once. A phased approach lets teams validate the design, fix data issues, and show value before expanding. A sensible first step is one high-value flow, such as sending process orders from ERP to MES and returning confirmations and material consumption. Once that is stable, introduce analytics on a single line or product family, then extend to other lines and sites.
The ISA-95 standard helps along the way. It defines the boundary and information exchange between enterprise systems and manufacturing operations systems, giving manufacturing, IT, engineering, and quality teams a shared vocabulary.
Building a Connected Manufacturing Environment
The real value of connecting ERP, MES, and analytics is continuity. Planning links to execution, execution feeds analysis, and the insights return to improve the next plan. For pharmaceutical manufacturers, that means better visibility, stronger traceability, and more confident process control.
Digital manufacturing isn’t about adding technologies one at a time. It is about making them work together so reliable information is available at the planner’s desk, on the shop floor, and in quality review.
Looking to connect your enterprise systems with manufacturing operations? Explore how ITRadiant’s SAP and digital transformation capabilities can help you evaluate integration opportunities and build a more connected manufacturing environment.
Add a Comment